-

Small busbar production process
Learn how copper busbars are manufactured, from raw material selection to cutting, stamping, CNC machining, plating, and final inspection for electrical and grounding systems. Whether you're planning a production line, optimizing your current setup, or simply understanding the busbar fabrication process. This article explains how copper busbars are manufactured in the UK. It gives a thorough explanation of the steps taken to turn raw copper into a finished conductor. This article will walk you through each critical stage of producing a bespoke copper bus bar, emphasizing the. Busbar manufacturing is the process of fabricating conductive strips, typically made from copper or aluminum, to distribute electricity efficiently in electrical busbar systems. These conductors are found in switchgear, control panels, busbar trunking, and high-capacity power distribution units. The process of busbar manufacturing involves cutting, bending, and drilling these metals into specific shapes and sizes to meet the precise requirements of various applications. Their design significantly reduces the space.
[PDF Version]
-
Production Process of Armored Fiber Optic Patch Cords
As a critical component in high-speed networks, fiber optic patch cords require micron-level precision. This guide unveils the complete production workflow compliant with **IEC 61754** and **Telcordia GR-326-CORE** standards, featuring proprietary quality control methods. Their performance directly impacts signal quality, insertion loss (IL), and return loss (RL). At Gcabling, our advanced manufacturing and strict quality control processes ensure. How to Make the Fiber Optic Patch Cords? - Elevating Your Project Profits with Superior Fiber Optic Patch Cords Producing high-quality fiber optic patch cords involves precise steps and procedures. Its main purpose is to form a flexible, high-performance link between active equipment and optical networking devices such as patch. Optical fiber pretreatment: fiber stripping, the introduction of professional fiber stripping tool, mainly for coating peeling, reduce the damage of the fiber cladding. For multi -mode fiber is concerned, this point is not affected, but the single mode fiber is concerned, the impact is relatively.
[PDF Version]
-
Wiring process for relay protection panels
This handbook covers the code of practice in protection circuitry including standard lead and device numbers, mode of connections at terminal strips, colour codes in multicore cables, dos and donts in execution. presentation of protection and control relaying. It covers standard codes, wiring practices, and norms for protecting generators, transformers, and lines, and provides detailed. Document converted into new template and updated throughout to reflect details of protection panels, relays and schemes currently in use. The copyright of this document, which contains information of a proprietary nature, is vested in Electricity North West Limited. The HT power supply is received from GO switch and distributed to the.
-

Customization Process for Low-Noise Fiber Bragg Gratings for Backbone Networks
Figure 1 illustrates the proposed reconfigurable grating. The grating consists of multiple series-connected uniform Bragg grating sections and a Fabry-Perot (FP) cavity section in the center of the grating. Each u.
-
Custom Process for Low-Noise Fused Tapered Brushed Molded Wires in Cloud Computing
Fused Filament Fabrication (FFF) is an Additive Manufacturing (AM) technique implemented in widespread applications and several components. Despite its benefits, the physics behind the FFF process is q.
-

Tanzania s butterfly optical cable production base
Raddy Fiber Manufacturing (T) Limited, a subsidiary of our parent company, is strategically located in Mwanambaya, a part of the Mkuranga district within the Coast Region, conveniently situated just 25 kilometers from Dar-es-Salaam. Our unwavering commitment revolves around the production of. The President of Tanzania Hon. The Tanzanian government is expected to soon begin exporting fiber optic cables to. Raddy Fiber Manufacturing Tanzania focuses on production of High Quality Fiber Optic Cables and its Accessories. The largest economy is Egypt, followed by South Africa, Ethiopia, Algeria and Nigeria. The Tanzania Fiber Optic Cable Market has been experiencing significant growth.
-

Domestic Production of Nanofiber Sensors
In this review, we focus on several nanofiber production methods as well as characterization methodologies to support the morphological, thermal, and mechanical characteristics under investigation.
FAQs about Domestic Production of Nanofiber Sensors
What is the current Nanofiber Market size?
The Nanofiber Market is projected to register a CAGR of greater than 15% during the forecast period (2023-2027). Read More
Who are the key players in Nanofiber Market?
eSpin Technologies Inc., Teijin Limited, TORAY INDUSTRIES, INC., NIPPON PAPER INDUSTRIES CO., LTD. and Hollingsworth & Vose Company are the major c...
Which is the fastest growing region in Nanofiber Market?
Asia-Pacific is estimated to grow at the highest CAGR over the forecast period (2023-2027). Read More
Which region has the biggest share in Nanofiber Market?
In 2023, the Asia-Pacific accounts for the largest market share in the Nanofiber Market. Read More
-
Optical Cable Coating Process Flow
Fiber optics technology has been applied into more and more varieties of specialty applications, where the optical fibers/cables are routinely used under harsh environments of high temperatures. The d.
-

Installation process of optical fiber cable in ducts
Installing duct fiber requires specialized techniques to navigate ducts (which may have bends, joints, or obstacles). The two most common methods are pulling and air blowing —each with unique advantages and use cases. The pulling method uses mechanical force to pull the cable. Corning Optical Communications cable specification sheets are available which list the maximum tensile load for various cable types. The installation process is influenced by local conditions, local climate, customer's existing procedures, and customer requirements. ulling has been the first technology for installing OF cables in duct. It. Where reels are supplied with protective material fitted over the cable, the protection should remain in place until the cable will be installed. The cable should be bent as little as possible.
[PDF Version]
-
654E Optical Cable Splicing Process
It describes three main splicing methods - de-matable connectors, mechanical splices, and fusion splices. Coherent optical technology and G. Sumitomo Electric Industries, Ltd. Through. Splicing with fusion splicers, in particular, has become an attractive method to quickly and easily connect fiber optic fibers. However, there are a few points to keep in mind during the. Fiber optic strands are ultra-lightweight and about as thin as human hair, and yet, they have more than eight times the pulling tension of a copper wire. E were introduced and have been extensively deployed worldwide. 1dB loss that will last the life of the cable plant.
-
Testing Process of Optical Module PMA4
In Section 4, we work through the key PAM4 optical and electrical compliance tests and conclude in Section 5 with a summary of the test equipment features and requirements that you need to debug PAM4.
-

Customized Process for Remote Monitoring of Quantum Communication MPO Adapter Modules
Modernization through secure, safe transition allows to overcome: Proprietary technologies that prevent network transparency in all aspects Obsolete technology processor preventing from improving.
-

Connection process between butterfly-shaped optical cable and prefabricated terminal
Fusion splicing is a popular method of connecting butterfly-shaped optical fiber cables. The two fiber cables are stripped of their protective coatings, and their bare ends are aligned and then fused together using a fusion. The utility model belongs to the technical field of communication equipment, in particular to a prefabricated end butterfly-shaped optical cable connector, which comprises an inner sheath, one end of the inner sheath is sleeved with an outer sheath in a sliding way, a sliding groove corresponding. Butterfly-shaped optical fiber cables are a popular type of fiber optic cable that is commonly used for data transmission in telecommunication networks. This design allows for easy installation and termination, as multiple fibers can be spliced or connected at once. In this. FTTH Butterfly Optic Cables are specifically designed to meet the growing demand for high-speed fiber-to-the-home deployments. The intraductal through -hole that is equipped with of backstop.
[PDF Version]
-

What are the main components of the optical module TX manufacturing process
Three main components make up the optical module: the external visible housing, the optoelectronic components, and the PCBA. Among them, transceiver design is the basis for optical transceiver production. It involves many fields such as optoelectronics and circuit design to ensure the performance and stability of. In the era of 5G, AI, and high-speed data centers, optical modules serve as the core bridge for converting electrical signals to optical signals (and vice versa), enabling fast, reliable data transmission across networks.
-
Norway Smart Distribution Cabinet Production
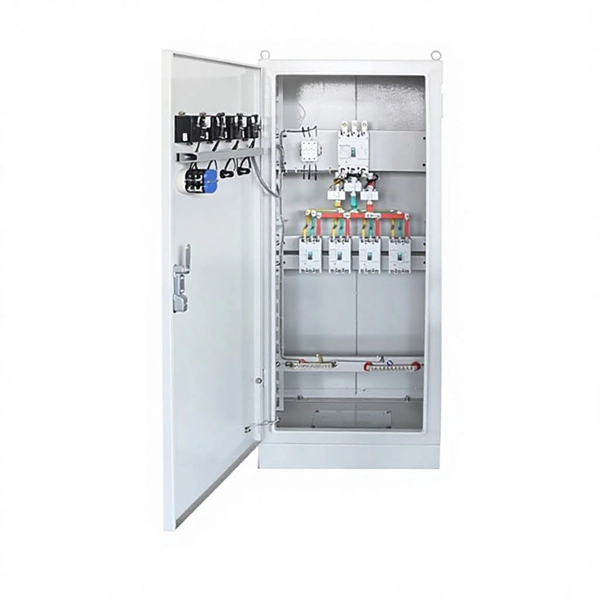
The companies Weidmüller, Komax, Zuken, Armbruster Engineering and nVent Hoffman / Steinhauer have launched the Smart panel building initiative in order to enable panel building to tap this potential with tailored, consistent solutions. With over 30 years of experience working with leading cabinet builders, Hatteland Technology offers extensive product knowledge, a comprehensive range of quality products and solutions, and a dedicated customer support center. Hatteland Technology is a Nordic manufacturer and supplier of industrial. ABB's Kabeldon cable distribution cabinets are a familiar sight in neighborhoods and by roadsides across Northern Europe, providing rugged all-weather protection for utility Low Voltage distribution systems. Our vision is to create one of Europe's most dynamic research alliances that brings together industry and research partners for the development of flexible and intelligent electrical energy systems.
[PDF Version]
-
How to weld ceramic ferrules
The stud is inserted into the chuck and - if necessary - equipped with a ceramic ferrule. A lift mechanism in the welding gun or welding head lifts the stud. A secondary arc (pilot arc) of low current is ignited between stud tip and work. Ceramic ferrules are used in stud welding as heat-resistant arc shields that contain molten metal, focus the arc energy, and protect the weld pool from atmospheric contamination during the drawn arc process. Learn more about ceramic ferrules and why they're so important in this blog. The process “Drawn arc stud welding” is used for studs of an approximate diameter of 3 to 25 mm, welding. Arc stud welding (ARC) with ceramic ferrule: The process drawn arc stud welding is mostly used for stud diameters of 3 to 25 mm and a welding time of 100 to 1 500 ms.
[PDF Version]